Door and Window High-Speed Extrusion Lines: How Can TPV Achieve Continuous Extrusion Without Breakage and Stable Dimensions?
Abstract
The door and window seal industry is gradually upgrading toward automation and high-speed extrusion, with mainstream line speeds continuously increasing. Many seal manufacturers report that ordinary TPV materials are prone to melt fracture and melt fluctuations under high-speed extrusion conditions, with large fluctuations in extruded cross-sectional dimensional tolerances, requiring frequent downtime for die head adjustment, resulting in low production uptime, limited capacity, and high scrap rates. Based on the production pain points of seal extrusion factories, this article analyzes the underlying causes of TPV melt fracture and dimensional instability under high-speed extrusion, introduces a high melt strength, low shrinkage TPV formulation solution, and provides supporting process optimization methods for extrusion lines, helping door and window seal manufacturers increase production speed, stabilize product dimensions, and reduce losses.
I. Pain Points in the Door and Window Seal Extrusion Industry: High-Speed Lines Stalled, Both Capacity and Yield Under Pressure
With the large-scale development of China's door and window industry, seal processing enterprises are continuously upgrading to high-speed extrusion production lines, aiming to increase single-line capacity and reduce unit processing costs. Conventional low-speed extrusion line speeds are 5–10 m/min, while new-generation high-speed lines have design targets of ≥25 m/min. However, after upgrading equipment, many factories encounter material adaptation challenges: general-purpose TPV materials cannot adapt to high-speed extrusion.
Typical production floor problems:
Extrusion melt fracture: During high-speed haul-off stretching, melt strength is insufficient, and the seal breaks at the die exit. Once breakage occurs, the line must be stopped to clean the die head and re-thread the material. A single downtime takes over ten minutes, disrupting production continuity and significantly reducing uptime.
Unstable cross-sectional dimensions: Large melt pressure fluctuations cause the seal cross-sectional thickness and width to vary, with dimensional tolerances exceeding the ±0.1 mm requirement. Non-conforming finished products can only be trimmed or reworked, increasing waste rates.
High process debugging difficulty: When changing material batches, melt flowability fluctuates, requiring re-adjustment of screw speed, haul-off speed, and die head temperature. This places extremely high demands on operator experience, resulting in unstable batch quality.
Breaking down the pain points across the industry chain:
Seal extrusion processing plants: High-speed line equipment requires high investment, but materials hold them back, preventing equipment capacity from being realized. Frequent downtime and increased waste drive up unit production costs; order delivery cycles are extended, affecting customer delivery. To improve stability, they must either choose expensive imported grades or continue using low-speed lines, falling into a dilemma.
Door and window finished product manufacturers: Fluctuations in seal cross-sectional dimensions cause poor fit between the seal and profile grooves during assembly, leading to assembly difficulties and uneven sealing contact, affecting overall window sealing performance. Dimensions that vary in size can also cause material jamming in automated assembly equipment.
Upstream TPV material suppliers: General-purpose TPV formulations focus on material elasticity while neglecting processing properties such as melt strength and molding shrinkage, failing to match downstream high-speed extrusion needs. Modifying to improve melt strength easily leads to deteriorated flowability and increased extrusion resistance, making formulation balance difficult.
Many factories attribute melt fracture and dimensional instability entirely to extrusion equipment and operator technical issues. However, extensive on-site verification shows that insufficient material melt strength and large shrinkage fluctuation are the core root causes of melt fracture and dimensional drift under high-speed extrusion conditions. Equipment optimization can only provide minor improvements; material formulation is the decisive factor.
II. Failure Mechanism of TPV in High-Speed Extrusion: Insufficient Melt Strength + Molding Shrinkage Fluctuation
During the extrusion molding process, TPV pellets are plasticized and melted by the screw, formed through the die head, continuously stretched by the haul-off machine, and cooled and shaped. Under high-speed conditions, the melt experiences higher tensile stress, and shortcomings in material processing characteristics are amplified.
Insufficient melt strength causes melt fracture: Melt strength represents the material's resistance to stretching in the molten state. General-purpose TPV has a relatively low base molecular weight and poor tensile strength in the molten state. At low extrusion speeds, the haul-off tension is small, and the problem is not obvious. When extrusion speed increases above 20 m/min, the molten seal emerging from the die exit is prone to melt tearing under haul-off tension, which is what the production floor calls melt fracture.
Molding shrinkage fluctuation causes cross-sectional dimensional drift: TPV undergoes crystallization shrinkage during cooling. If shrinkage rates differ between material batches, or if melt temperature fluctuations cause shrinkage rate changes, the cross-sectional dimensions of the seal will change after cooling and shaping. During high-speed extrusion, cooling time is short, shrinkage is uneven, and dimensional tolerances are difficult to control, making it hard to consistently maintain tolerances within ±0.1 mm.
Uneven plasticization aggravates fluctuations: General-purpose TPV formulations have melt viscosity sensitive to temperature. Slight changes in screw shear cause severe melt pressure fluctuations, and die head discharge varies, further amplifying dimensional fluctuations. High-speed extrusion involves stronger shear, making localized overheating and uneven plasticization more likely.
Factories attempt to simply reduce haul-off speed. Although this can reduce melt fracture, it sacrifices the capacity advantage of high-speed lines, greatly reducing equipment investment returns. Therefore, to unleash the potential of high-speed lines, it is necessary to optimize melt performance starting from the TPV material formulation.
III. Dedicated TPV Technical Solution for Door and Window Extrusion: High Melt Strength + Low Shrinkage Formulation, Compatible with ≥25 m/min Extrusion Lines
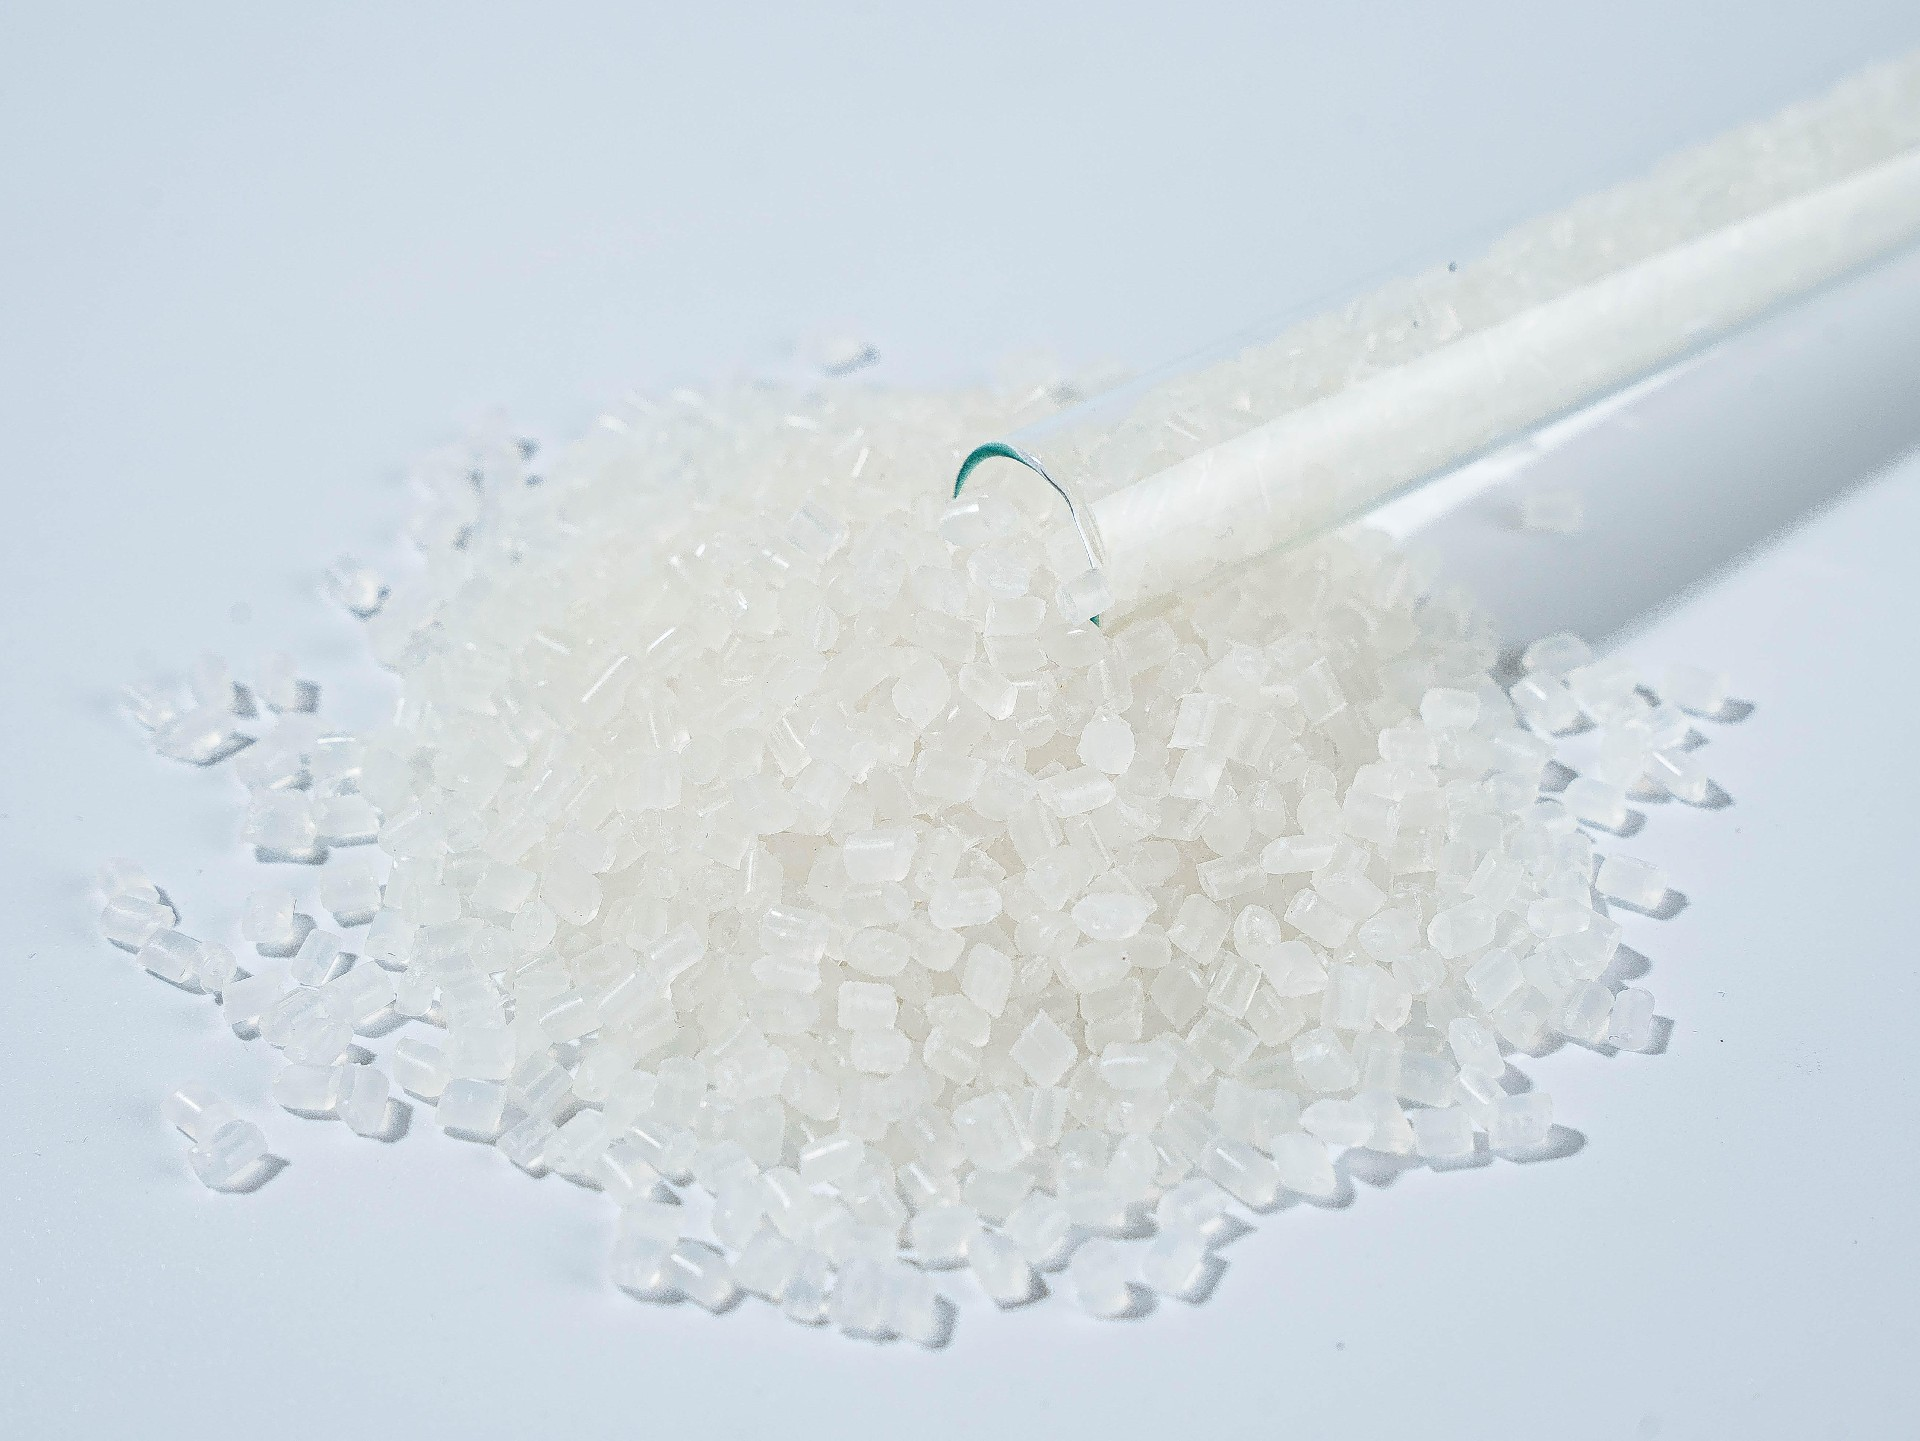
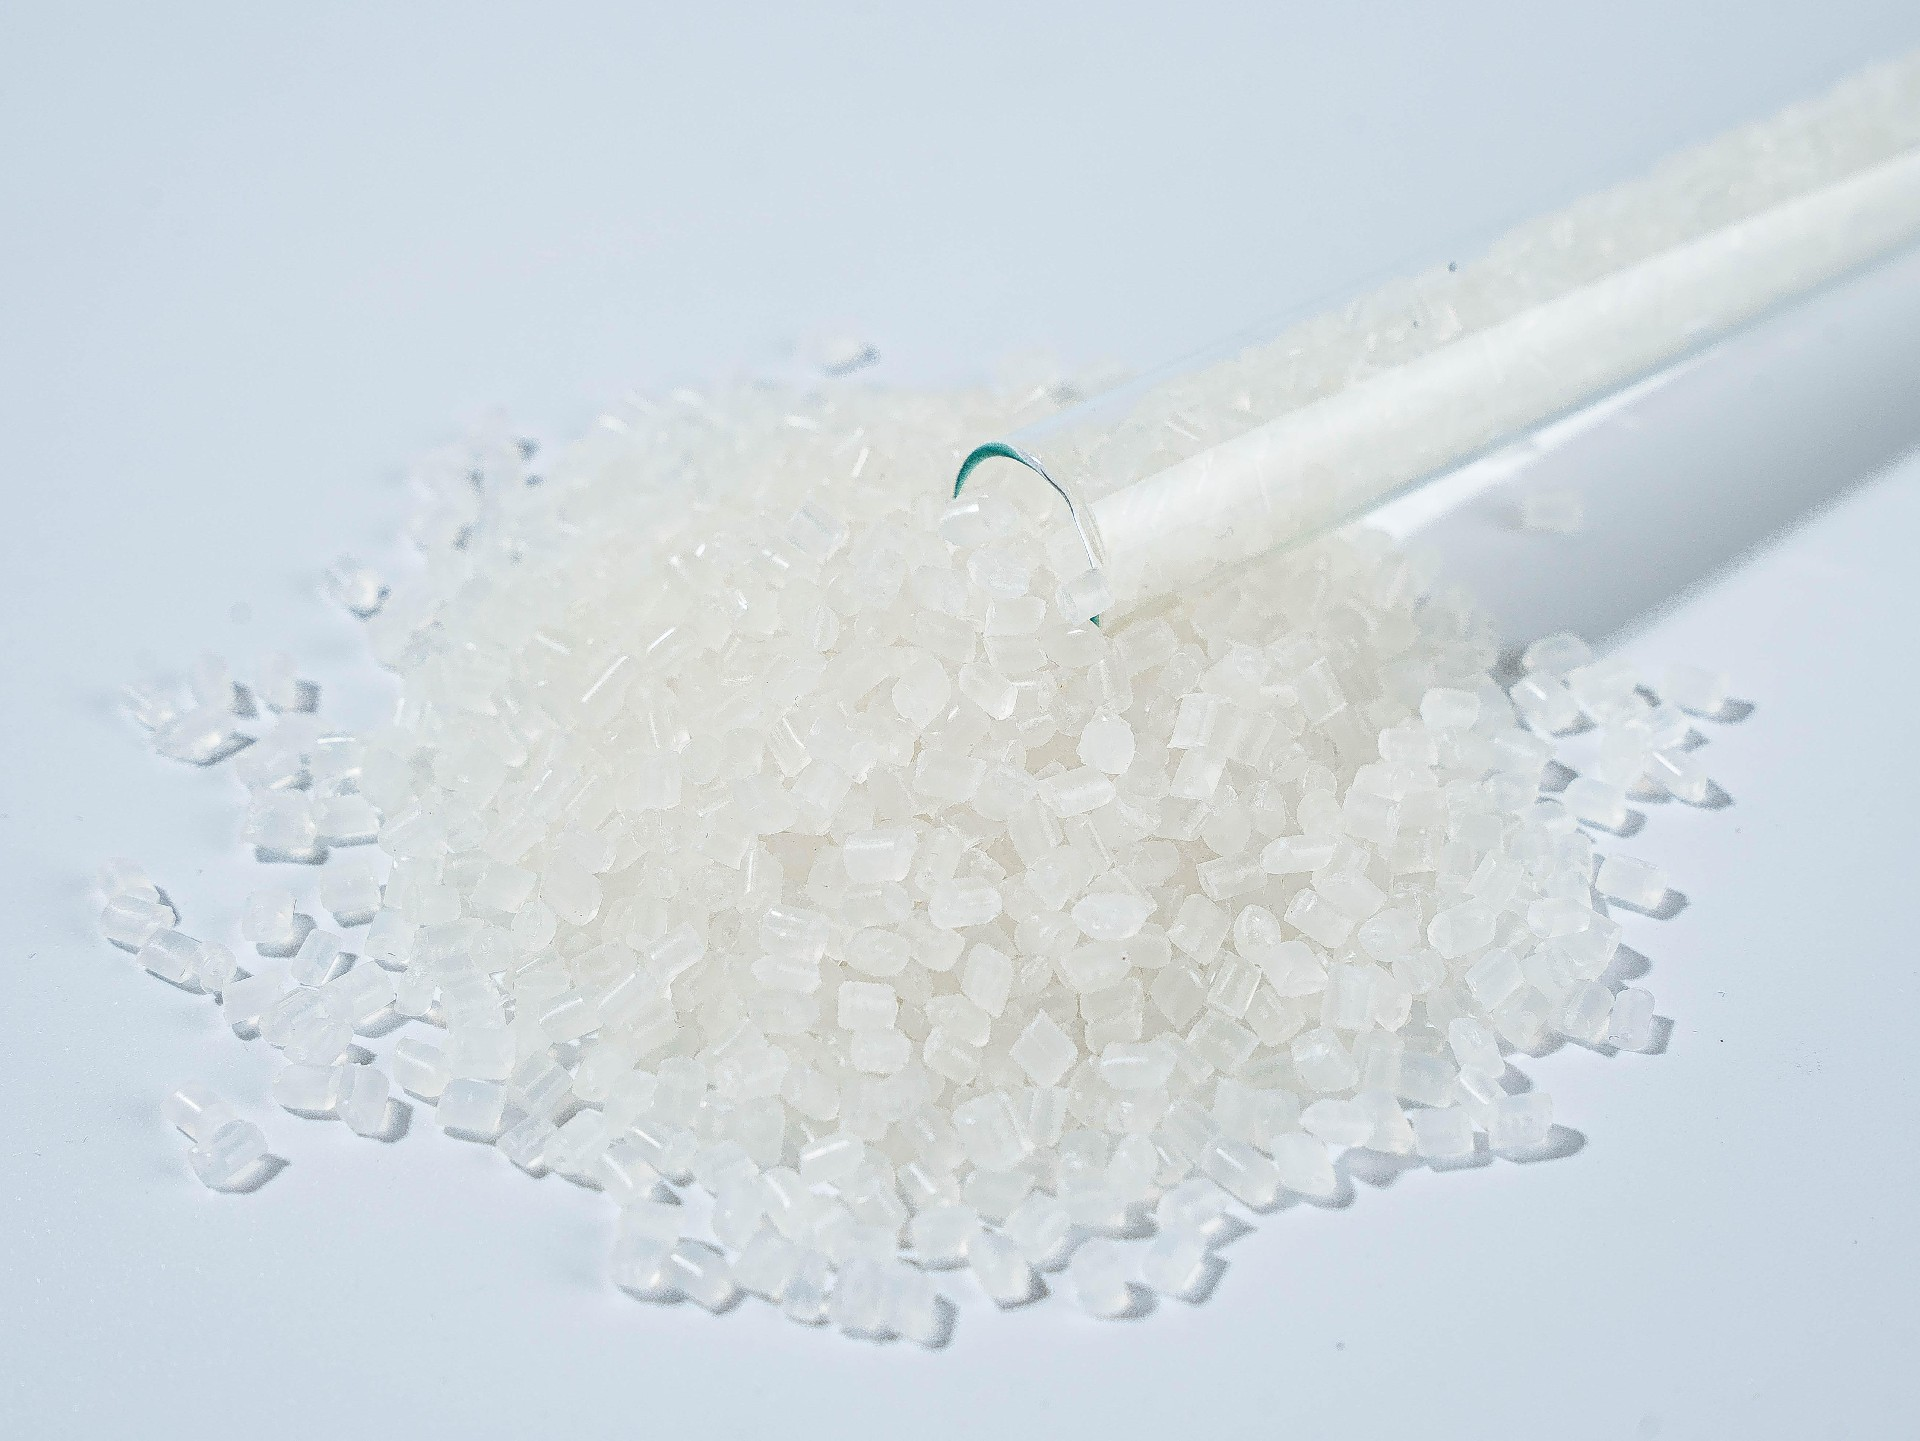
The core of dedicated TPV formulation design for door and window high-speed extrusion: balance melt strength, melt flowability, and molding shrinkage to ensure continuous extrusion without breakage under high-speed haul-off and stable dimensions after cooling.
High molecular weight polyolefin base modification: Select high molecular weight base resin to improve melt strength in the molten state, enhancing the die exit melt's resistance to tensile tearing, making it less prone to breakage under high-speed haul-off. At the same time, control molecular weight distribution to avoid excessive extrusion pressure caused by deteriorated flowability.
Stable crosslinked rubber phase system: Optimize the EPDM dynamic crosslinking process. The rubber phase structure is uniform and stable, reducing the sensitivity of melt viscosity to temperature and shear rate. Over a wide shear range, melt flow is more stable, and die head discharge pressure fluctuations are small.
Low shrinkage controllable formulation system: Add nucleation control components to uniformly control crystallization rate, reduce molding shrinkage, and narrow shrinkage rate differences between batches. The seal cooling and shaping process shrinks uniformly, and cross-sectional dimensional fluctuations are controlled.
Corresponding performance: The dedicated TPV grade for door and window high-speed extrusion can achieve stable production at extrusion line speeds ≥25 m/min with no melt fracture during production; extruded seal cross-sectional dimensional tolerance ≤±0.1 mm; strong batch-to-batch consistency of raw materials, with factory uptime increased to over 95%, greatly reducing downtime for debugging.
Soft placement: This dedicated extrusion TPV grade is developed specifically for door and window seal high-speed lines, with a wide processing window, compatible with existing single-screw extrusion equipment, requiring no large-scale modification of die heads and screws, reducing factory equipment modification costs.
IV. Supporting Process Optimization Solution for High-Speed Extrusion Lines
Quality materials are the foundation. Combined with process optimization, the performance of high-speed TPV can be maximized.
4.1 Raw Material Pretreatment
TPV materials should be dried and protected from moisture. Moisture absorption in raw materials can cause extrusion bubbles, and bubble locations become weak points in the melt, inducing melt fracture under high-speed haul-off. Control warehouse humidity and inspect incoming materials for caking or moisture.
4.2 Extruder Temperature and Screw Parameter Debugging
High melt strength TPV has a wider processing window. Set temperatures according to the recommended range; do not excessively increase barrel temperature. Excessive temperature reduces melt strength and actually makes melt fracture more likely. Debug screw speed and haul-off speed in a coordinated manner to establish a stable speed ratio and reduce haul-off tensile stress fluctuations.
4.3 Cooling and Shaping System Upgrade
During high-speed extrusion, seal cooling time becomes shorter, and the sizing water tank length and water temperature need to match the extrusion speed. Ensure uniform cooling to avoid shrinkage differences caused by uneven localized cooling, which can lead to seal distortion and dimensional deviation. Regularly calibrate sizing dies to reduce dimensional errors caused by die wear.
4.4 Online Monitoring During Production
Install online dimensional inspection devices to monitor seal cross-sectional dimensions in real time. When dimensional deviation occurs, adjust parameters promptly to reduce batch non-conforming products. Maintain production records, fix raw material grades and process parameters, and reduce debugging workload when changing batches.
V. Industry Summary: Door and Window Seal Industry Upgrade—Material Adaptation to High-Speed Manufacturing Is an Inevitable Trend
Automation and high-speed operation in the door and window seal industry is a major trend. Many enterprises have completed hardware equipment upgrades, but material support cannot keep up, causing high-speed lines to "run slowly." General-purpose TPV can only adapt to low-speed extrusion. To realize the value of high-speed lines, dedicated TPV grades for door and window extrusion must be selected.
Upstream TPV material manufacturers need to extend their R&D focus from static mechanical indicators of materials to processing rheological properties, providing downstream extrusion plants with rheological data and processing guidance solutions to achieve material-process synergy. Midstream seal extrusion processing plants should add high-speed extrusion trial verification during the procurement evaluation stage, not only testing finished seal mechanical properties, but focusing on melt fracture conditions, dimensional stability, and continuous production uptime, incorporating processing performance into raw material admission standards. Door and window brand customers should pay attention to seal production stability during supply chain selection. Stable dimensional control ensures automated assembly efficiency and improves overall window sealing consistency.
High melt strength, low shrinkage TPV solves the two major production pain points of melt fracture and dimensional drift in high-speed extrusion, helping seal enterprises unleash high-speed line capacity, reduce waste and downtime losses, achieve cost reduction and efficiency improvement, and adapt to the development direction of large-scale intelligent manufacturing in the door and window industry.